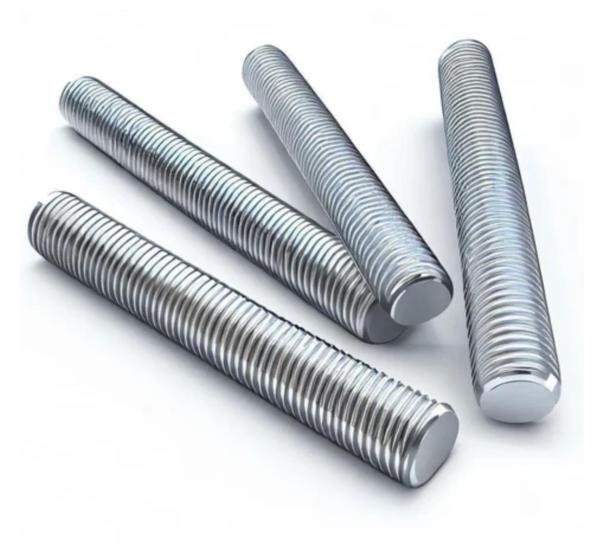
Our Threaded Rods are manufactured across a full range of strength classes and finishes for anchoring, suspension, and general fastening applications — supplied fully threaded, or as tap-end, double-end, full-bodied, and undercut studs to suit the assembly.
- Grades
- 4.6 / 4.8 (Mild Steel), 8.8 (High Tensile), A2/304 & A4/316 (Stainless), ASTM A193 B7, ASTM A307/A36
- Finishes
- Plain / Bare Steel, Zinc Plated (BZP/ZP), Hot Dip Galvanized (HDG), Stainless Steel (304 or 316)
- Standards
- ISO 724, ISO 268, ISO 68-1, ASME B1.13M, ASME B1.1, BS 3643, BS 84
- Inch Sizes
- 1/4" to 8"
- Metric Sizes
- M6 to M152
- Imperial Threads
- BSW, ASME, BSF
- Metric Threads
- ASME, ISO
- Formats Available
- Fully Threaded Rod, Tap-End Studs, Double-End Studs, Full-Bodied Studs, Undercut Studs
Mechanical Properties by Grade
| Grade | Standard | Tensile Strength (min) | Yield / Proof Strength (min) | Hardness |
|---|---|---|---|---|
| 4.6 | ISO 898-1 | 400 MPa (58 ksi) | 240 MPa (35 ksi) | ≈114–209 HB |
| 4.8 | ISO 898-1 | 420 MPa (61 ksi) | 340 MPa (49 ksi) | ≈124–201 HB |
| 8.8 (d ≤ 16mm) | ISO 898-1 | 800 MPa (116 ksi) | 640 MPa (93 ksi) | ≈235–320 HB |
| A2-70 / A4-70 | ISO 3506-1 | 700 MPa (102 ksi) | 450 MPa (65 ksi) | ≤ 220 HB |
| ASTM A193 Gr. B7 | ASTM A193 | 860 MPa (125 ksi) | 720 MPa (105 ksi) | 19–35 HRC |
| ASTM A307 Gr. A | ASTM A307 | 414 MPa min (60 ksi) | Not specified by std. | — |
| ASTM A307 Gr. B | ASTM A307 | 414–689 MPa (60–100 ksi) | Not specified by std. | — |
Reference values per published ISO 898-1 / ISO 3506-1 / ASTM A193 / ASTM A307 standards. Mill test certificates available on request for any order.
Types We Manufacture
Same product, five end-configurations — chosen by how and where the rod engages with the assembly.
Fully Threaded Rod
Threaded end-to-end with no head (also called continuous thread or all-thread) — cut to any length on site, ideal where the engagement point isn't fixed in advance.
Best for: Cut-to-length anchoring & suspension workTap-End Stud
Short thread on one end for screwing into a tapped hole, with a longer nut-end thread on the other — common on valve bonnets, flanges, and machinery casings.
Best for: Valve bonnets, flanges & machinery casingsDouble-End Stud
Equal thread length at both ends with a plain center section, secured with a nut on each side — both ends usually chamfered for easy engagement.
Best for: Joining two components with equal reachFull-Bodied Stud
Shank diameter matches the thread's major diameter, keeping stress concentrated in the threads rather than the shank — suited to higher static load joints.
Best for: High static-load structural jointsUndercut Stud
Shank machined down to the thread's pitch diameter so stress is shared more evenly between shank and thread — preferred for fatigue and cyclic-load applications.
Best for: Fatigue-prone, cyclic-load connectionsApplications & Industries Served
Structural Steel Fabrication & Bridges
Used as tie rods, bracing, and connection hardware in structural steel frames and bridge trusses, where high-tensile grades carry sustained load and vibration.
HVAC, MEP & Pipe Suspension Systems
Suspends ductwork, cable trays, and pipe runs from ceiling slabs — zinc-plated or galvanized finish is the standard choice for long-term indoor corrosion resistance.
Solar & Renewable Mounting Structures
Anchors ground-mount racking and rooftop solar arrays to their foundations, where hot-dip galvanized or stainless rods stand up to years of outdoor weather exposure.
Oil, Gas & Process Piping
Used as flange and valve-bonnet stud bolts (typically ASTM A193 B7 with A194 nuts) across pressure piping, valves, and process equipment in refineries and gas plants.
Precast Concrete Anchoring
Cast into precast panels and tilt-up walls as anchor points and lifting inserts, forming the connection back to structural steel on site.
Power Transmission Towers & Substations
Bolts lattice tower members and busbar/equipment supports together, almost always hot-dip galvanized for decades of outdoor service.
How Our Threaded Rods Are Made
Raw Material Selection
Certified low-carbon, alloy, or stainless steel wire rod, chemically tested before it enters production.
Thread Rolling
Threads are cold-rolled rather than cut, giving a smoother finish and higher fatigue strength than a cut thread.
Heat Treatment
Quenching and tempering for high-tensile grades (8.8, ASTM A193 B7) to reach the required strength and hardness.
Surface Finishing
Plain, zinc-plated, hot-dip galvanized, or stainless passivation — applied per the finish ordered.
Inspection & Testing
Dimensional, thread-gauge, and mechanical (tensile / proof-load) checks before anything is packed.
Custom Cutting & Packing
Cut-to-length service on request, then export-ready bundling and labeling.